|
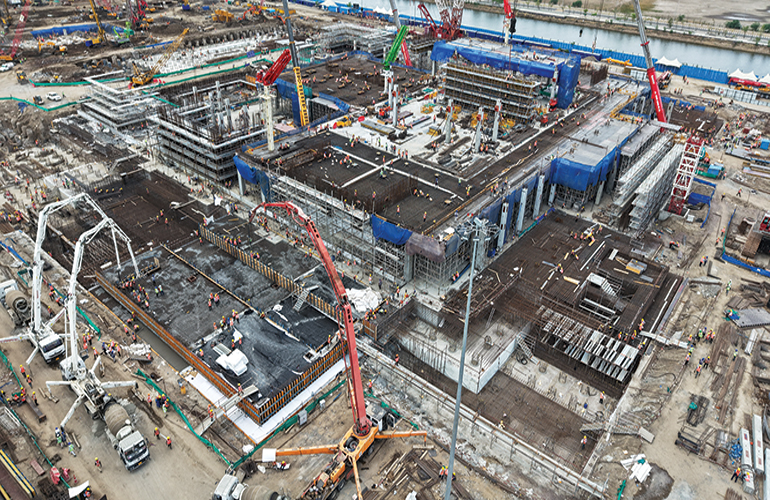
The momentous concrete pour in progress.
L&T marks major milestone for India’s first semiconductor manufacturing facility Remarkable project milestones come in all sizes. A single concrete pour of 4,458 cubic metres was completed on 16 June for the raft foundation of India’s first semiconductor manufacturing facility, being developed by Tata Semiconductor Manufacturing Pvt Ltd at Dholera, a planned greenfield ‘smart’ city in Gujarat. This feat was achieved by L&T’s Buildings Infrastructure – Residential, Commercial Buildings & Factories vertical. This logistically complex operation was completed smoothly despite challenging site conditions and tight constraints. The continuous concrete pour over a 48-hour window, maintained an average concreting rate of 93 cu m per hour through four simultaneous pumping arrangements, utilising three boom placers and one static pump. The team also achieved its highest-ever daily concrete pouring quantity of 3,250 cu m. This was executed through seamless coordination of three in-house batching plants, supplemented by an external Ready Mix Concrete plant, demonstrating exceptional planning and resource optimisation. Notably, this milestone was achieved while simultaneously executing major concrete activities in other project areas like piles, showcasing the team’s remarkable execution strength. This milestone achievement builds upon the project team’s sustained performance over the past six months, during which 2,64,772 cu m of concrete was placed through effective planning, coordination and execution. The facility is coming up across a 163-acre site. The project’s first phase comprises a built-up area of 1,46,738 sq m and is being constructed by L&T Construction as a first-of-its-kind facility in the country. This phase will support technology nodes from 110/90 nm down to 28 nm, with 55 nm as the start-up node. At full build-out, the project will feature 32,000 sq m of cleanroom space with a production capacity of 50,000 wafer starts per month. The record concrete pour affirms L&T’s high level of professionalism and project management.
|
|
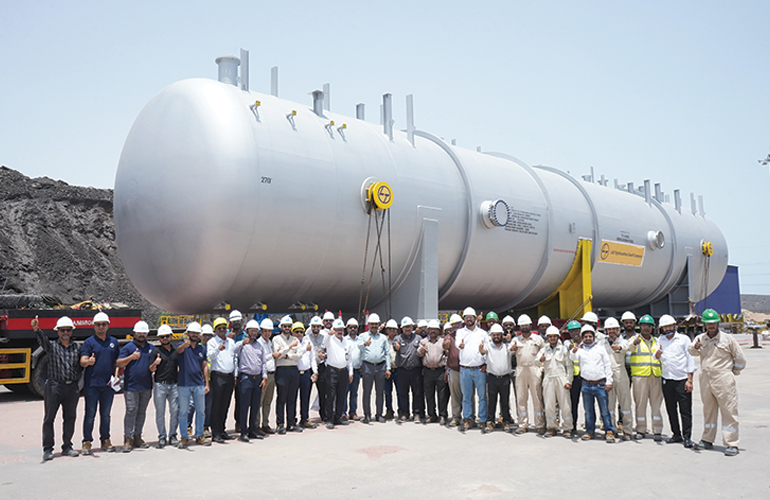
The L&T team and representatives of the customer, Saudi Arabian Oil Company, with the 300 MT vessel.
L&T Heavy Engineering marks a momentous despatch from its Saudi Arabian facility The completion of a project is always a cause for jubilation – both for the customer and for the project team. One such success was the despatch of the 300 MT depressurising vessel in May from L&T Hydrocarbon Saudi Integrated Manufacturing Factory, i.e. the Heavy Wall Pressure Vessel facility at Jubail in the Kingdom of Saudi Arabia. The vessel was bound for the Jafurah Gas Compression Project (Phase II). Fabricated by the L&T Heavy Engineering team, the vessel is approximately 7 metres in diameter and nearly 40 metres in length. It is among the largest to have been dispatched since the facility began manufacturing vessels in October 2024. In recognition of this accomplishment, representatives from the customer, Saudi Arabian Oil Company, visited L&T’s facility to commend the exceptional efforts and dedication of the L&T team for their unwavering support, commitment and contribution to this success. The world-class facility undertakes advanced manufacturing. In a short span of time, it has secured Aramco 9COM approvals (6000002522, 6000002523, 6000002524 & 6000002525) and is supporting key projects in the region. Accredited with ASME U, U2, S, R and NB along with ISO 9001 : 2015, 14001, 45001, 29001 certifications, the facility delivers end-to-end capabilities - from design to dispatch. It is equipped with cutting-edge infrastructure to undertake complex fabrication, giving reliable support to the region’s industries. The facility has the capacity to manufacture equipment using a wide range of materials. Importantly, L&T’s facility focuses strongly on the development of local talent, equipping Saudi Arabia’s Gen-Z with the skills required to participate in boosting the economy and take the people of the Kingdom to even greater heights of prosperity. A definite win-win!
|
|
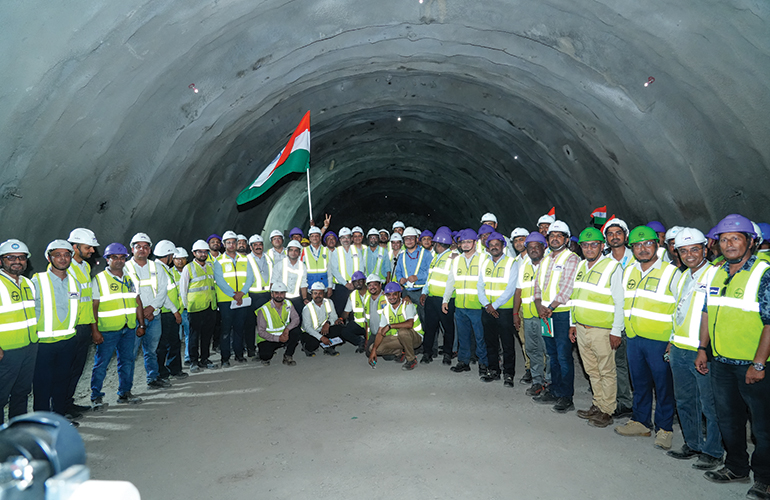
The triumphant tunnelling team at Ambesari village in Maharashtra’s Palghar district.
A momentous breakthrough on the Mumbai-Ahmedabad Bullet Train Corridor project India’s first Bullet Train project has achieved a construction milestone – the breakthrough of Mountain Tunnel 7. This momentous development took place on 1 June, marking the project’s third such breakthrough within a five-month span. The event was witnessed by Dr Hemant Vishnu Savara (Member of Parliament for the Palghar Lok Sabha Constituency), Anjum Pervez (MD, National High-Speed Rail Corporation Limited [NHSRCL]), G Vinod (EVP & Head of Operations, Mumbai-Ahmedabad High-Speed Rail [MAHSR] C4 & C3 and Dubai HSR), Zamshed Ali (Task Force Leader Head, MAHSR C3), Dipak Roy (Principal CPM, NHSRCL) and other key officials from NHSRCL, the Project Management Consultancy consortium (led by Tata Consulting Engineers) responsible for overseeing civil construction and L&T.
Located at Ambesari village within the Sahyadri mountain range in Dahanu Taluka, the 417-metre-long 12.6-metre-wide tunnel was engineered to accommodate both up and down tracks. The tunnel was excavated from both sides over 516 days and through 117 controlled blasts, using the New Austrian Tunnelling Method, an advanced technique allowing for real-time monitoring of geological conditions and the immediate deployment of site-support systems, as well as shotcrete, rock bolts and lattice girders. Strict safety protocols were maintained – including ventilation, fire prevention and controlled access arrangements. Safe excavation was ensured by advanced real-time tunnel instrumentation monitoring systems and state-of-the-art monitoring tools – such as 3D targets, seismographs and surface settlement points – marking a first-of-its-kind deployment in the Indian Railways. The MAHSR C3 project comprises 135.45 km of elevated section between Silphata in Thane and Zaroli on the Maharashtra-Gujarat border and three stations (Thane, Virar and Boisar) with 124 km of viaduct, including 101 km of 2,584 full span launching method girders, and 17 km to be built using segmental and underslung segmental launching girders. The section also features 2.3 km of steel bridges and additional structures – including 6 km through seven mountain tunnels – and 5 km of special earth structures. The successful breakthrough reflects the engineering excellence, technical capability and sheer dedication of the MAHSR C3 project team working in demanding terrain.
|
|
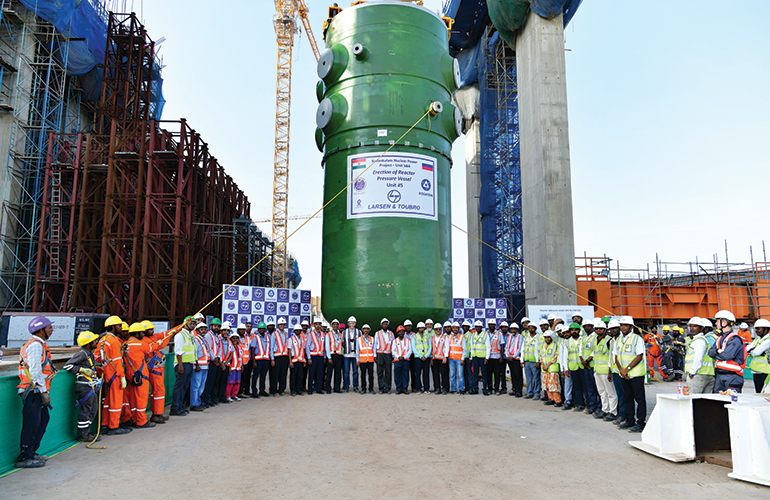
The reactor pressure vessel towers over L&T’s project team at Kundakulam Nuclear Power Project.
L&T’s Heavy Civil Infrastructure team marks a significant achievement An important construction milestone was reached on the Kundakulam Nuclear Power Project (KKNPP) on 15 June. The reactor pressure vessel was erected for its Unit 5 (2 x 1000 MWe) by L&T’s Heavy Civil Infrastructure business. The vessel is the heart of the nuclear reactor. It houses the reactor core, fuel assemblies, control rods and key internal components where nuclear fission generates the thermal energy required for power production. Serving as the primary safety barrier within the Nuclear Steam Supply System (NSSS), the vessel is among the most safety-critical and precision-engineered components of a nuclear power plant. Supplied by Rosatom, Russia, the VVER-1,000 vessel is an engineering marvel. It weighs 320 MT, stands 11.185 m high and has a diameter of 4.69 m. Designed to operate under extreme conditions of 321°C temperature and 160 bar pressure, it has a service life exceeding 60 years. The installation of this behemoth is a testament to L&T’s engineering excellence, meticulous planning, and flawless execution. Completed with Zero Harm and a First Time Right approach, the activity involved detailed lift planning, precision alignment, stringent quality controls and seamless coordination across multiple functions while adhering to the highest nuclear safety standards. Demonstrating exceptional execution quality, the team achieved an v flange flatness of 78 microns against the specified tolerance of 100 microns – the best alignment result achieved across KKNPP Units 1 to 5. KKNPP Units 5 & 6 Mechanical Erection Package comprises the installation of critical reactor and turbine island systems, including the reactor pressure vessel, steam generators, main coolant systems, turbine-generator package, seawater systems, cranes, piping, structural steel works and auxiliaries. This accomplishment reinforces L&T’s leadership in executing complex nuclear projects and highlights its enduring commitment to safety, quality, innovation and engineering excellence. It is yet another example of how L&T continues to contribute to India’s energy security and the nation’s growing clean energy ambitions.
|
|
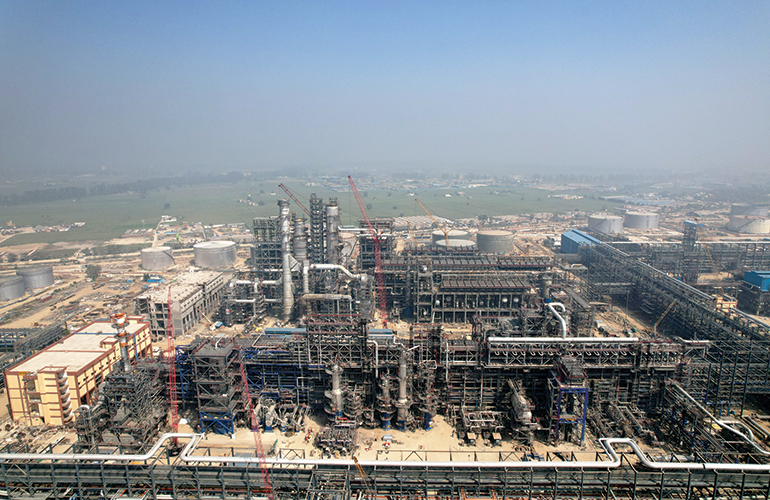
The Diesel Hydrotreater Unit will produce 5 million metric tonnes of cleaner fuel every year, lowering vehicular emissions.
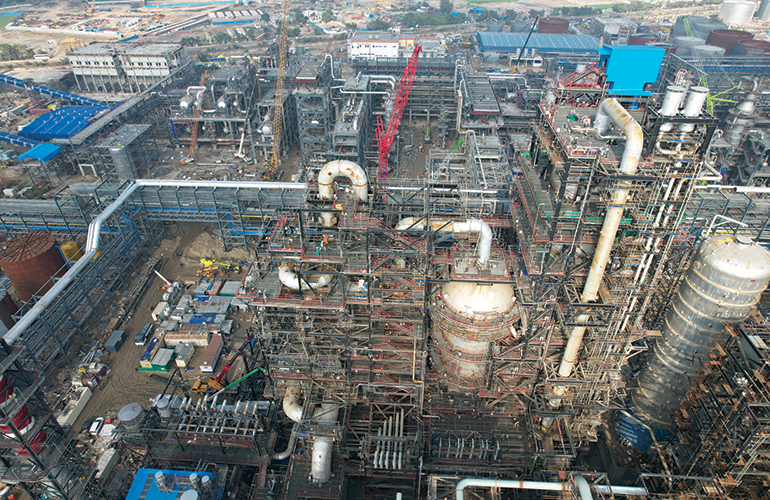
Every year, the Rx-Rg will convert 2.5 million metric tonnes of crude fractions into higher-value products.
L&T Energy Hydrocarbon Onshore achieved twin milestones on a major project L&T’s Energy Hydrocarbon (LTEH) Onshore has achieved two major mechanical completion milestones at Indian Oil Corporation Limited’s (IOCL) Panipat Refinery Expansion Project in Haryana, i.e. • The 5 Million Metric Tonnes Per Annum (MMTPA) Diesel Hydrotreater (DHDT) Unit on 29 May • The 2.5 MMTPA Reactor-Regenerator (Rx-Rg) System Package of the INDMAX Fluid Catalytic Cracking (FCC) Unit on 11 June These achievements reinforce L&T’s capability to deliver complex refinery projects through engineering excellence, innovation and flawless execution while contributing significantly to India’s energy security and cleaner fuel aspirations. Awarded by IOCL, both projects were executed on a comprehensive Engineering, Procurement and Construction basis. The scope encompassed project management, process engineering, detailed engineering, procurement, fabrication, inspection and testing, transportation, construction, pre-commissioning, commissioning support, performance guarantee testing and successful handover. While the DHDT Unit is licensed by Shell, the Rx-Rg package is based on Lummus Technology’s globally licensed INDMAX process developed by IOCL’s R&D Centre. The DHDT Unit is designed to produce premium-quality Bharat Stage VI (BS-VI) compliant diesel through advanced hydrotreating technology, helping reduce vehicular emissions while meeting India’s growing demand for cleaner fuels. The diesel produced will be suitable for use in extreme climatic conditions, including temperatures as low as -15°C, enabling uninterrupted fuel supply to India’s armed forces deployed in challenging terrains such as Siachen Glacier, Ladakh and Jammu & Kashmir. The unit is India’s largest single-train Diesel Hydrotreater licensed by Shell. The Rx-Rg System Package converts heavy crude fractions into higher-value products, using advanced catalytic cracking technology. Based on IOCL’s indigenous INDMAX technology, licensed globally by Lummus Technology, the unit is designed to maximise LPG production, aligning with India’s rapidly increasing LPG demand and supporting the Government of India’s Pradhan Mantri Ujjwala Yojana, which provides deposit-free LPG connections to women from poor and deprived households. Delivering these projects demanded exceptional planning, coordination and innovation. The DHDT team executed a complex 1,350 km multimodal transportation operation involving sea and road movement of oversized equipment from Hazira to Panipat, overcoming challenging terrain and infrastructure constraints. The largest consignment was 36 metres long, 8 metres wide and weighed 626 metric tonnes. The team erected the Hydro Desulphurisation Reactor within just 36 hours of its arrival at site and pioneered the implementation of the Free Issue Material philosophy for critical equipment. Proactive pre-commissioning activities accelerated overall project readiness. The Rx-Rg project presented an equally demanding execution landscape. Procurement involved complex imports under the Manufacturing and Other Operations in Warehouse Regulations scheme, while construction was carried out within a highly congested plot with multiple contractors working simultaneously. Six Over Dimensional Cargo (ODC) equipment weighing over 500 metric tonnes each were fabricated and erected within five months. The project achieved the first-ever site fabrication of ODC equipment for IOCL. Innovation and digitalisation played a critical role across both projects. L&T leveraged integrated digital platforms to improve productivity, enhance quality and strengthen project control. The Rx-Rg project also introduced sustainable construction practices by adopting pneumatic testing instead of conventional hydrotesting for refractory-lined piping, conserving approximately 26.8 lakh litres of water. Robotic arc welding and Leica laser tracker-enabled bolt matching further enhanced precision and construction efficiency. Safety and quality remained at the core of execution. The DHDT project recorded 9.6 million safe workhours, while the Rx-Rg project achieved over 5.85 million safe workhours, reflecting L&T’s uncompromising commitment to Health, Safety and Environment. Both projects earned multiple prestigious recognitions from the Confederation of Indian Industry, the World Safety Organisation and other industry bodies for excellence in safety performance. The projects maintained outstanding quality standards, achieving excellent customer satisfaction scores, industry-leading audit ratings and exceptionally low weld repair percentages. A defining aspect of these achievements was the leadership demonstrated by L&T’s young workforce. With an average team age of approximately 33 years and 13% women representation at the frontline, both projects showcased the capability of L&T’s emerging leaders in executing some of India’s most complex refining infrastructure. The projects exemplified the strength of L&T’s integrated ecosystem, bringing together expertise from L&T Onshore EPC, AdVENT (Advanced Value Engineering & Technology), Heavy Engineering, L&T Valves, CarbonLite Solutions and specialised lifting teams to deliver world-class outcomes. The mechanical completion of these two strategic refinery units marks an important milestone in the project, strengthening L&T’s position as a trusted engineering, procurement and construction partner for India’s most critical energy infrastructure. This will result in the production of cleaner fuels, increase LPG availability and contribute significantly to India’s long-term energy security and sustainability goals.
|
|
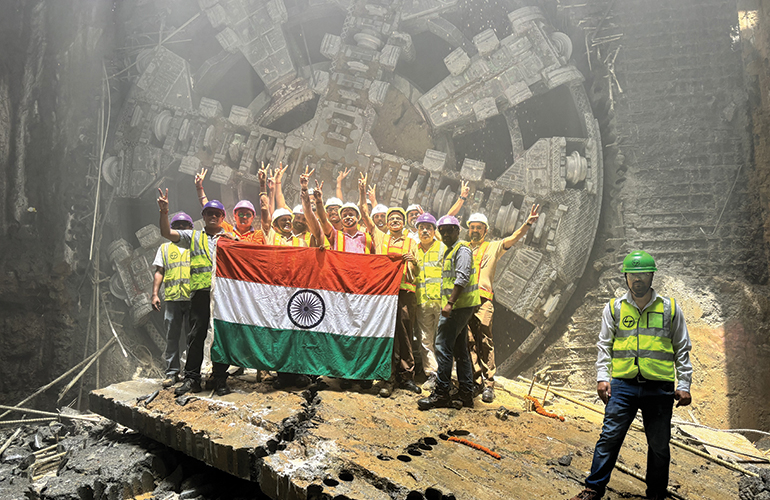
The victorious L&T Heavy Civil Infrastructure tunnelling team in Patna.
L&T’s Heavy Civil Infrastructure team touches a double highpoint Two tunnel breakthroughs are indeed a feat! This was achieved by L&T’s Heavy Civil Infrastructure team on the Patna Metro project in June. The two tunnel-boring machines (TBMs) tunnelled in parallel, with a 100 m lag, from Moin-Ul-Haq Stadium Station towards Rajendra Nagar Station, each excavating approximately 700 m before breaking through the diaphragm wall at Rajendra Nagar Station. This marks yet another significant achievement in the execution of the project’s underground works.
This stretch posed a formidable array of engineering and operational challenges. The alignment required tunnelling beneath active railway tracks, navigating through densely built neighbourhoods with heritage structures, and advancing through complex mixed geological strata along a steep tunnel gradient. Mixed soil below sub-nominal groundwater levels further intensified the risk, compounded by the need to break through diaphragm walls interlaced with intricate municipal utility networks at the headwall. The team meticulously optimised TBM parameters, while maintaining continuous monitoring of both surface and subsurface instrumentation. Round-the-clock vigilance by a multidisciplinary Emergency Response Team ensured uncompromised safety and precision. A defining achievement was the drama beneath the highly congested railway corridor at Rajendra Nagar Terminal, part of the critical Delhi-Howrah mainline, which sees nearly 108 train movements daily – including premier semi-high-speed services such as Vande Bharat, Namo Bharat, Tejas and Rajdhani Express. The feat was accomplished through close coordination and effective teamwork among officials of East Central Railway, Delhi Metro Rail Corporation (DMRC) and Patna Metro Rail Corporation (PMRC) and L&T. Special permission was secured from Indian Railways to temporarily restrict train speeds to 10 km/h over a 24-day window, enabling the TBMs to execute a flawless 80m-long crossing beneath 5 railway lines and 4 platforms, while maintaining tunnel-induced ground settlement within the exceptional limit of under 4 mm. The breakthroughs were graced by Sandeep Kumar R Pudkalkatti (Secretary UDHD-cum-MD, PMRC) and S N Joshi (PD – DMRC). The project team was represented by Aloke Kumar Dey (Project Director), Monu Govil (Dy Project Manager) and Arvind Kumar Tyagi (DPM – Tunnel). The officials appreciated the efforts of the project team in overcoming the challenging conditions to achieve this milestone.
|
Follow javascript: SP.SOD.executeFunc('followingcommon.js', 'FollowDoc', function() { FollowDoc('{ListId}', {ItemId}); }); 0x0 0x0 ContentType 0x01 1100 Compliance Details javascript:if (typeof CalloutManager !== 'undefined' && Boolean(CalloutManager) && Boolean(CalloutManager.closeAll)) CalloutManager.closeAll(); commonShowModalDialog('{SiteUrl}'+
'/_layouts/15/itemexpiration.aspx'
+'?ID={ItemId}&List={ListId}', 'center:1;dialogHeight:500px;dialogWidth:500px;resizable:yes;status:no;location:no;menubar:no;help:no', function GotoPageAfterClose(pageid){if(pageid == 'hold') {STSNavigate(unescape(decodeURI('{SiteUrl}'))+
'/_layouts/15/hold.aspx'
+'?ID={ItemId}&List={ListId}'); return false;} if(pageid == 'audit') {STSNavigate(unescape(decodeURI('{SiteUrl}'))+
'/_layouts/15/Reporting.aspx'
+'?Category=Auditing&backtype=item&ID={ItemId}&List={ListId}'); return false;} if(pageid == 'config') {STSNavigate(unescape(decodeURI('{SiteUrl}'))+
'/_layouts/15/expirationconfig.aspx'
+'?ID={ItemId}&List={ListId}'); return false;}}, null); 0x0 0x1 ContentType 0x01 898 Document Set Version History /_layouts/15/images/versions.gif?rev=40 javascript:SP.UI.ModalDialog.ShowPopupDialog('{SiteUrl}'+
'/_layouts/15/DocSetVersions.aspx'
+ '?List={ListId}&ID={ItemId}') 0x0 0x0 ContentType 0x0120D520 330 Send To other location /_layouts/15/images/sendOtherLoc.gif?rev=40 javascript:GoToPage('{SiteUrl}' +
'/_layouts/15/docsetsend.aspx'
+ '?List={ListId}&ID={ItemId}') 0x0 0x0 ContentType 0x0120D520 350
|
|
|